Topic: Manufacturing Processes
In a butt welding process using arc welding, the arc power is found to be 2.5 KVA. The process is used to weld two steel plates each of 3 mm thickness as shown in the figure. Determine maximum possible welding speed. It is assumed that the metal transfer is a short circuit type and the arc is on for 85% of the total time. Take alpha_steel = 1.2 x 10^-5 m²/s, k_steel = 43.6 W/m C, melting point of steel = 1530 C and ambient temperature = 30 C
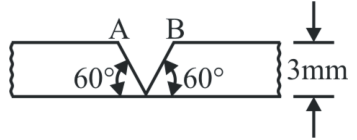
- A. 0.035 m/s
- B. 0.0146 m/s
- C. 0.02 m/s
- D. .0156 m/s
Answer: D. .0156 m/s
Explanation: Given the arc-on time efficiency is 0.85, the effective heat input rate is Q = 0.85 * 2500 W = 2125 W. The width of the weld pool for the given geometry is w = 2 * t * tan(30) = 2 * 3 * (1/$\sqrt{3}$) = 2 * $\sqrt{3}$ mm. Using the welding heat equation: Q = 8 * k * (Tm - Ta) * t * (1/5 + (v * w) / (4 * alpha)). Substituting values gives 2125 = 8 * 43.6 * (1500) * 0.003 * (0.2 + (v * 2 * $\sqrt{3}$ * 10^-3) / (4 * 1.2 * 10^-5)). Solving for the velocity v yields approximately 0.0156 m/s.